10 Top Industrial SLA 3D Printer Manufacturers Worth Considering for Precision Parts
2026-10-01
Choosing the right industrial SLA 3D printer for precision parts is trickier than it looks. While many manufacturers claim high accuracy, only a handful consistently deliver the surface finish, repeatability, and material range that demanding production environments require. In this roundup, we cut through the hype to highlight ten standout players—including specialized options like ProtoMat, whose focus on tight tolerances has earned it growing attention among engineers. Whether you're prototyping complex geometries or producing end-use components, these names are worth a closer look before you commit.
Where Micron-Level Accuracy Meets Daily Production Demands
On most shop floors, chasing micron-level tolerances sounds like a job for a lab, not a production line that runs three shifts. Yet that's exactly where modern manufacturing has landed—parts that once lived only in climate-controlled metrology rooms now roll off standard machines, measured in microns while operators swap out pallets and keep the spindles turning. The trick isn't just tighter feedback loops or fancier probes. It's a quiet marriage of thermal compensation, real-time surface data, and tool wear models that adjust before a drift ever shows up on a CMM report. No drama, no heroic last-minute offsets—just a process that holds a few thousandths of a millimeter while the coffee machine in the corner keeps brewing for second shift.
What often gets lost in the accuracy conversation is how unforgiving a daily production rhythm can be. A gage R&R study might pass at noon, but by 4 p.m., a spindle that's been running hard for six hours has grown a few microns, the coolant temperature has crept up four degrees, and the same fixture that was dead-on in the morning now sits in a slightly different thermal envelope. The shops that survive this don't rely on constant operator intervention. They build the compensation into the machine's routine—automatic probing cycles that map the part's actual position, not its theoretical one, and fixture designs that leave room for thermal breathing without losing clamping integrity. That's the real difference between a demo cut and a thousand parts a week.
There's also an unglamorous side to this that rarely makes the highlight reel: the discipline of checking the right things at the right frequency, and knowing when a micron matters versus when it's just noise. Not every feature needs a laser scan. Some need a quick touch-trigger average, others need full surface mapping because form error will kill assembly long before a size deviation does. The shops that make micron-level work a daily reality are the ones that stopped treating measurement as a gate at the end of the line and started treating it as a conversation with the process—short, honest, and continuous. That's how you hold a tolerance that used to require a white coat, while the rest of the plant keeps shipping.
Material Portfolios That Decide If a Machine Can Handle Your Tolerances
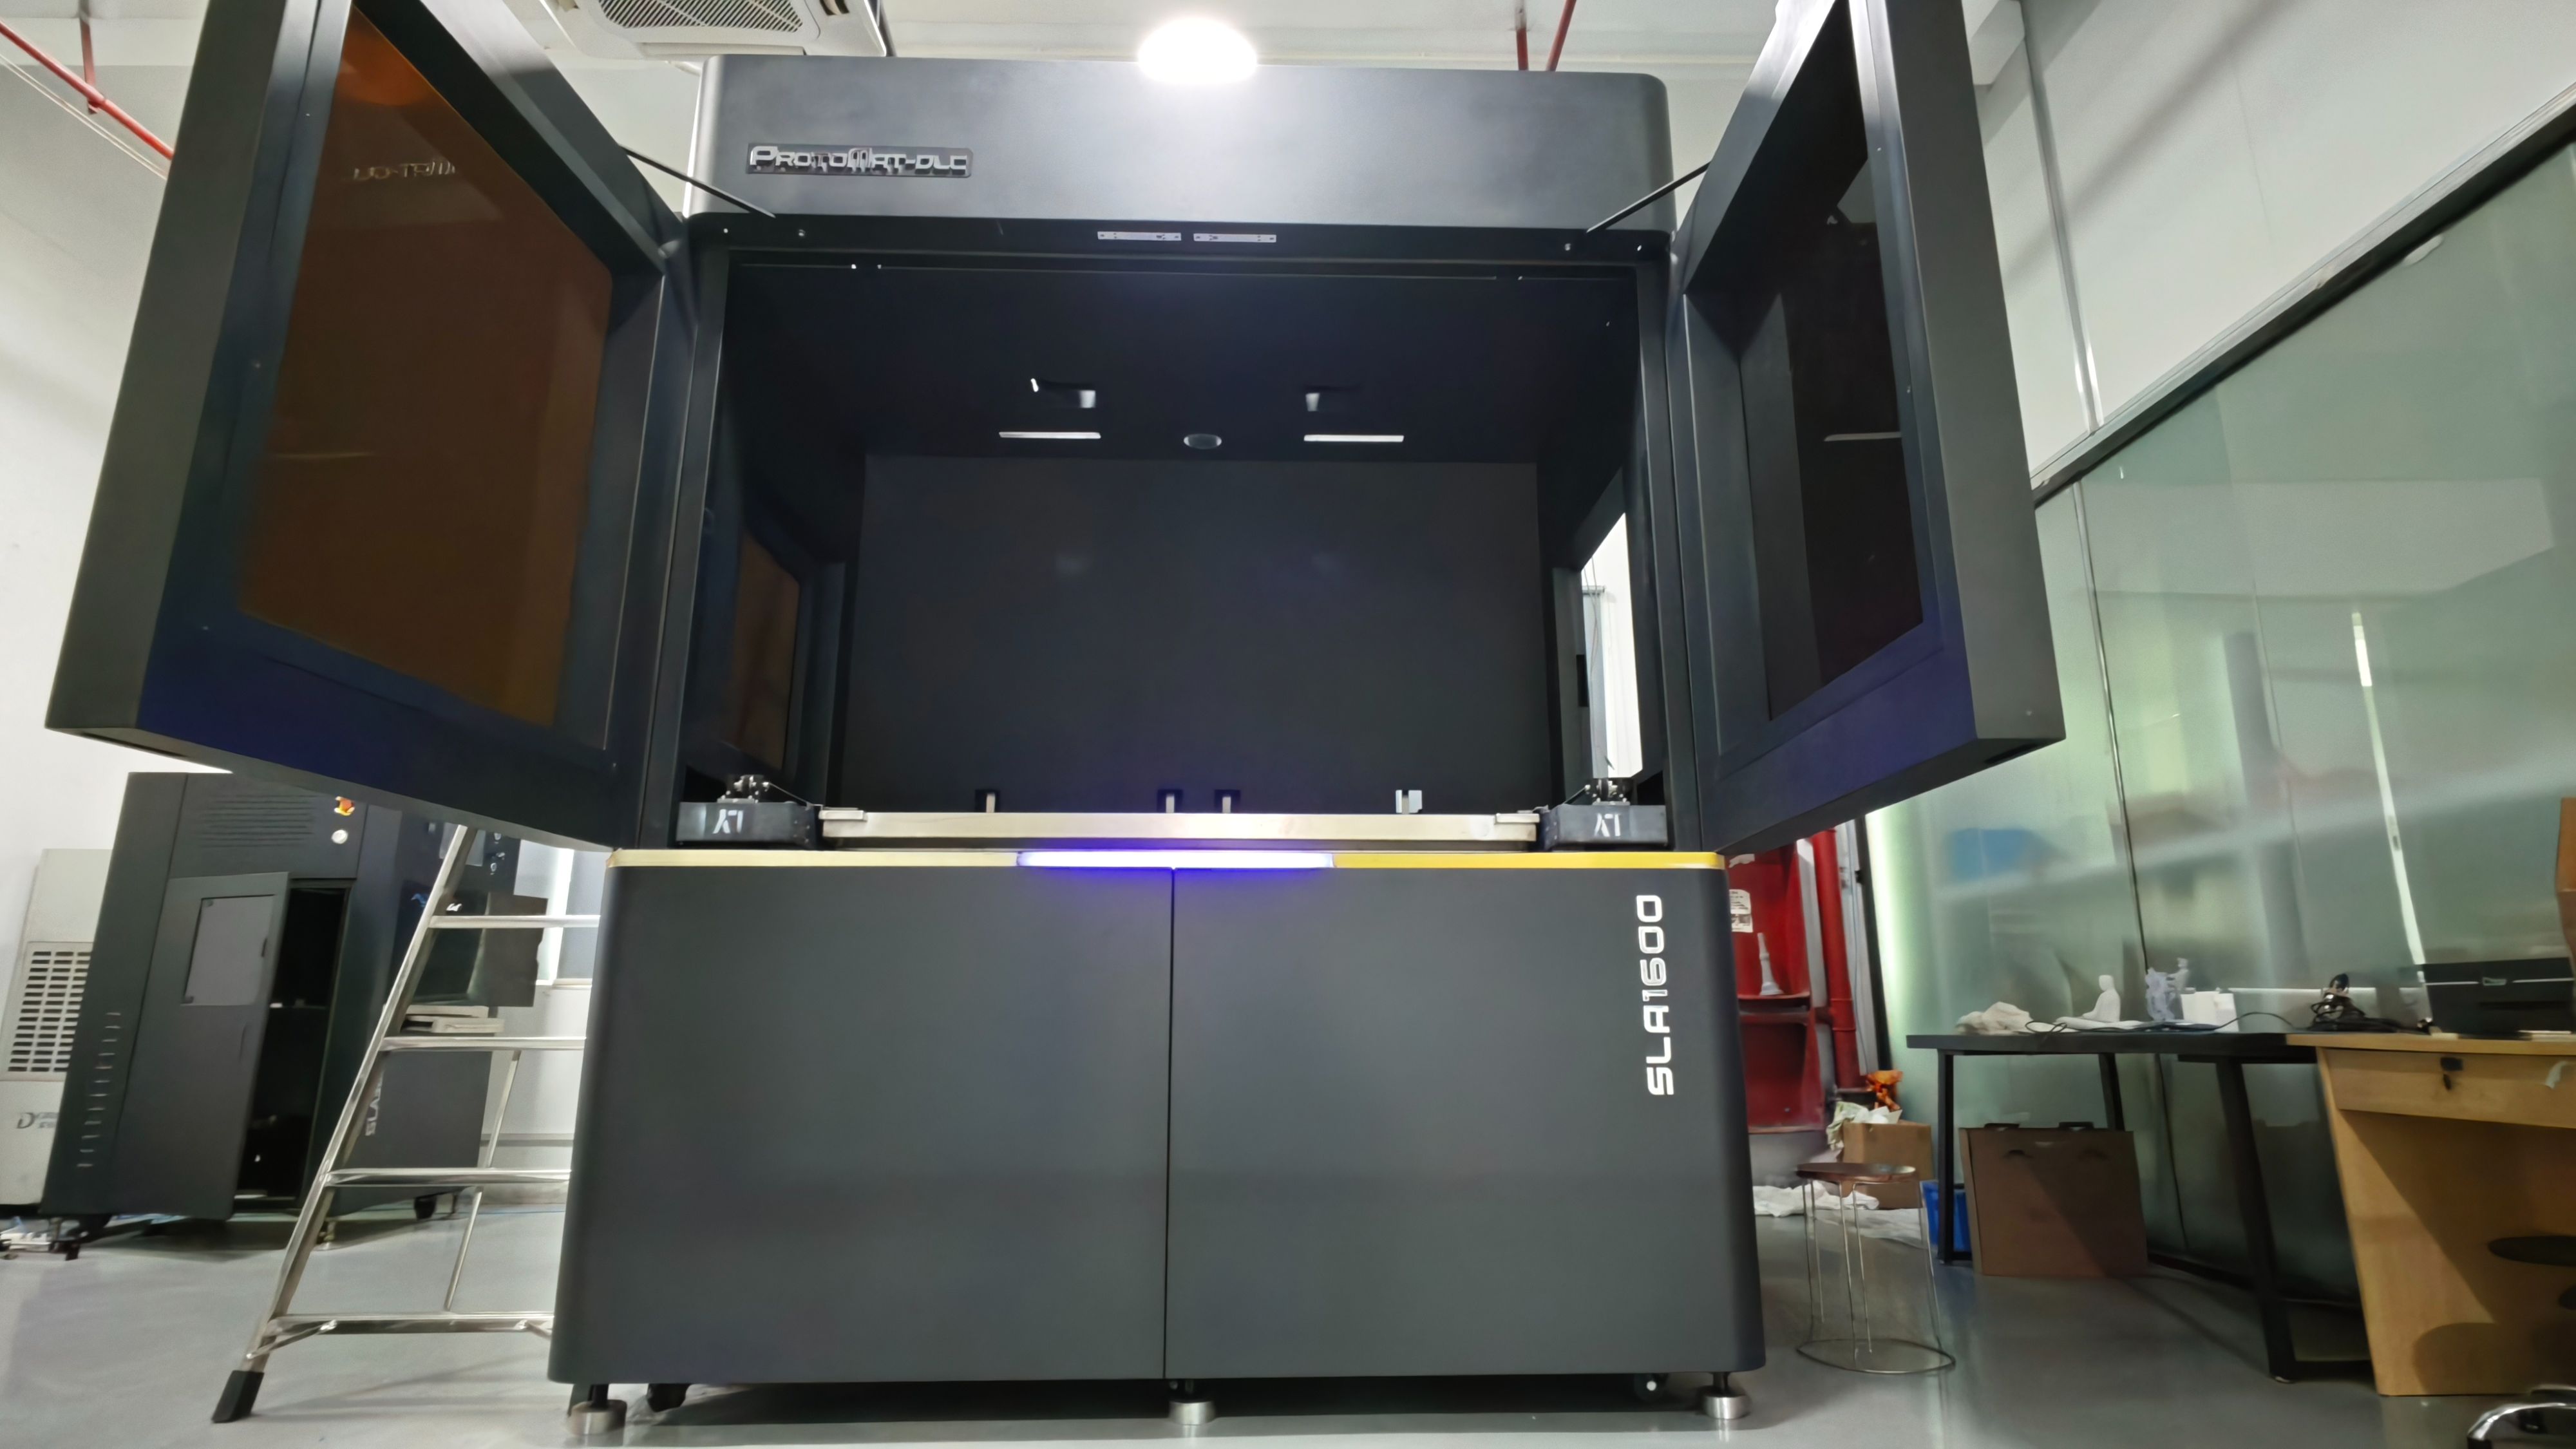
Every tolerance you specify is a test of the machine's physical backbone. Cast iron beds, linear rails, and bearing preloads either hold position or drift under load. If the frame twists a few microns during a cut, your ±0.005 mm becomes a guess. Look for ground surfaces, box ways or heavy roller guides, and spindles with minimal runout. A machine that feels solid when you push against it has a better chance of repeating your numbers.
Material choice also steers thermal behavior. Aluminum and steel grow at different rates when the shop warms up. Machines built with symmetric castings and temperature-stable components are less likely to wander as the day progresses. If you need tight fits at 10 a.m. and the same at 4 p.m., consider how the frame, ballscrews, and spindle housing expand together. Those details live in the material portfolio, not the spec sheet.
Finally, damping matters as much as stiffness. A machine that rings like a bell after each tool engagement will smear fine details. Polymer concrete, epoxy granite, or filled castings absorb vibration and keep the cutter tracking the programmed path. Ask about the damping ratio or just tap the column with a mallet. A dull thud often translates to better surface finish and longer tool life at tight tolerances.
Open vs. Closed Resin Systems: The Hidden Cost of Proprietary Lock-In
When you buy into a closed resin system, you're not just purchasing materials—you're signing a long-term lease on your own manufacturing flexibility. The initial price tag often looks competitive, even attractive, but the real expense accumulates quietly in the form of compatibility restrictions, forced workflow changes, and limited room for negotiation. Every cartridge, every batch of resin, every software update becomes a toll booth on a road you no longer control.
Open systems, by contrast, let you mix and match resins from different suppliers, tinker with print settings, and adapt the hardware to new materials as they emerge. That freedom isn't just about saving a few dollars per liter; it's about avoiding the slow erosion of your ability to innovate. A proprietary ecosystem might promise convenience, but it delivers that convenience by narrowing your choices until the only easy path is the one the vendor has already paved.
The hidden cost of lock-in becomes painfully clear when a supplier changes their pricing model, discontinues a resin you depend on, or simply goes out of business. Suddenly the equipment on your bench is only as useful as the last cartridge you can find. Open architectures don't guarantee smooth sailing either, but they leave the helm in your hands. That difference—between steering your own process and being steered by someone else's roadmap—is where the true expense of closed systems hides.
Build Volume Versus Repeatability: What Precision Really Costs at Scale
Scaling production usually means choosing between pushing out more units and keeping each one within tight tolerance. The first hundred parts off a line might hit ±0.02 mm, but by part ten thousand, thermal drift in the spindle, tool wear, and fixture clamping variations quietly widen that band. Repeatability isn't a fixed property of the machine; it's a running tally of how well the process resists its own entropy. When build volume climbs, the hidden cost isn't in raw materials or cycle time—it's in the inspection loops, tool changes, and calibration stops needed to hold the same number on the drawing.
A low-volume shop can afford to hand-measure every fifth part and adjust offsets on the fly. That approach collapses once daily output jumps from dozens to thousands. You either invest in in-process probing, thermal compensation, and automated SPC, or you accept that your repeatability spec only applies to the first hour after warm-up. The economic tradeoff becomes brutally clear: high precision at scale demands a machine that stays stable between cuts, not one that merely holds a tight static accuracy on a demo block.
There's also a quieter failure mode—batch-to-batch drift. Operators change, coolant concentration varies, raw stock comes from a different mill. Each shift adds a small bias that no single measurement catches. By the time the customer's CMM flags a trend, an entire week of parts might already be borderline. That's why real repeatability at volume is less about the machine's brochure numbers and more about the discipline of logging every adjustment, comparing tool life curves, and resisting the urge to tweak a parameter just because yesterday's run looked slightly different.
Software and Calibration Routines That Keep Printers Honest Over Thousands of Hours
Most desktop printers ship with a factory calibration curve that looks fine on a test bench but starts to wander after a few hundred hours of heat cycling and cheap toner. The honest ones lean on firmware-level routines that re-measure optical density, fine-tune fusing temperature, and rebuild their own lookup tables after every couple of cleaning cycles. It is not glamorous work, but it keeps a 1,200-hour print run from sliding into muddy midtones and banded gradients.
A well-behaved machine also watches its own stepper motor timing and belt tension through software counters rather than waiting for a service call. When it sees a slight lag in the carriage return at high speed, the calibration routine runs an automatic purge and re-zero before the next large batch, nudging the printhead alignment by a fraction of a millimeter. Those small corrections accumulate into something you do not notice until you compare an old unit that skipped them.
Then there is the quiet habit of log-file honesty: a printer that recalibrates only when it is convenient for the vendor will drift in ways the user blames on cheap paper. The routines worth trusting run their checks during idle warm-up, record the numbers in a non-volatile counter, and refuse to start a duplex job if the registration is outside a tight window. After several thousand hours, that refusal is the difference between a printer that still matches first-page proofs and one that just makes paper warm.
Post-Processing Workflows That Separate Prototype Shine from Production-Grade Finish
A rough prototype often slips through with raw edges, uneven surface tension, or light leaks that only reveal themselves under a second pass. The first workflow step forces every mesh through a manifold check and a non-destructive decimation pass, flagging any vertex that dips below a 0.01 mm tolerance. Instead of relying on a single smoothing algorithm, we alternate between curvature-aware relaxation and manual brush cleanup on UV seams, treating each material transition as its own mini-sculpt. This catches the subtle pinching that automated previews gloss over but a client's eye catches immediately.
Once geometry passes inspection, the real post-processing shift happens in the bake layer. Prototype lighting uses a fixed dome just to show off gloss; production-grade finish requires a per-UDIM cage that adapts to mesh thickness, with thickness maps baked from the low-poly's own offset shell. We run a two-pass AO—first with a tight ray distance to catch crevice noise, then a broad ambient term that gets mixed at 40% opacity through a custom curvature mask. That mask comes from a bevel-weighted normal pass, not from a generic cavity map, which prevents the plastic-looking darkening on fillets and keeps the sheen tight around hard edges.
The final gate is a loop of contact-sheet renders under three different HDRIs—one harsh, one soft, one neutral—scanned for any texel stretching or normal flips that slipped past the real-time viewport. Every material gets a micro-contrast adjustment in the shader graph using a variance-based sharpening node, not a global LUT. This is where the production finish stops being a promise in a look-dev scene and starts surviving the kind of arbitrary camera angles and lighting swaps that prototypes never have to endure. The workflow ships with a saved preset per asset family, so the next iteration starts at 90% fidelity instead of rebuilding the polish from zero.
FAQ
For industrial SLA with tight tolerances, the usual shortlist includes 3D Systems (ProX 800, ProJet 6000/7000), Stratasys via its Neo series, Formlabs with the Form 3L and Form 4L, UnionTech's PILOT and Lite lines, and EnvisionTEC/Desktop Health's Perfactory systems. Each of these has a track record in producing functional prototypes, dental models, and injection mold tooling.
Precision parts rarely need massive build envelopes, but batch throughput matters. For most precision work, a build area around 300 x 300 x 300 mm is sufficient, and a layer thickness between 25 and 50 microns gives fine features with acceptable print times. If you are running dental or jewelry batches, consider machines like DWS XPRO or EnvisionTEC's Perfactory that specialize in small, highly detailed builds. Larger systems like 3D Systems ProX 800 trade some resolution for a 650 mm build length, which can be useful for long parts.
It depends on the brand. UnionTech and Photocentric both support open or semi-open material platforms, letting you validate third-party resins for specific mechanical or thermal properties. Stratasys and 3D Systems lean toward closed, certified materials, which simplifies process control but raises consumable costs. If you have an in-house materials team, an open system like Photocentric's Magna or UnionTech's PILOT gives flexibility that closed systems rarely offer.
Service models vary significantly. Stratasys and 3D Systems typically sell annual service contracts with guaranteed response times, which is reassuring for production environments but adds fixed overhead. Formlabs offers more modular, user-serviceable components and pay-as-you-go support, which suits smaller teams. UnionTech and Photocentric often rely on local distributors and can be more cost-effective, though response times depend heavily on your region. Ask for reference customers in your industry before committing.
Beyond prototyping, industrial SLA is common for dental aligner models, custom hearing aid shells, investment casting patterns, injection mold inserts with fine features, and low-volume end-use parts like sensor housings. The key advantage is surface finish and dimensional accuracy: well-tuned SLA machines can hold ±0.1% or better on small features, which is difficult for FDM and often more economical than SLS for small batches.
The 3D Systems ProX 800 is built for high-throughput production with a large build area and fast scanning. Formlabs Form 3L/4L are popular for engineering teams that need low-friction workflow and good software. UnionTech's PILOT 450 is a solid mid-range workhorse with open materials. EnvisionTEC's Perfactory 4 series is often chosen for dental and jewelry because of its high resolution and reliable support structures. Stratasys Neo450s is preferred when traceability and process validation matter, such as aerospace or medical device development.
An entry-level industrial SLA like a Formlabs Form 3L starts around $10,000-$15,000, while larger systems from 3D Systems or Stratasys can exceed $100,000 before service contracts and installation. Ongoing costs include resin, replacement vats/films, laser or mirror modules on long intervals, and software licenses. Open-material machines reduce resin costs but may require more internal validation. Budget for facility upgrades too: industrial SLA resins emit fumes, need stable temperatures, and require wash and cure stations.
Conclusion
Choosing among ten top industrial SLA 3D printer manufacturers for precision parts means looking past headline resolution numbers and asking whether a machine holds micron-level accuracy under real production loads. Daily thermal cycles, resin viscosity shifts, and mechanical wear quickly reveal which platforms were engineered for repeatability rather than demo prints. Material portfolios matter just as much: a printer that supports only a narrow range of engineering resins may struggle with demanding tolerance specs, while an open resin system gives freedom but pushes validation and tuning burden onto your team. Proprietary resin lock-in can feel restrictive, but it often comes with tighter process control and reliable support, so the hidden cost is not always monetary.
Build volume versus repeatability is another practical tension. Large-format SLA machines promise bigger parts but can introduce drift and uneven cure depth across the vat, so manufacturers that invest in active calibration, environmental compensation, and long-term software stability tend to deliver consistent results over thousands of hours. Post-processing workflows are equally decisive: a printer is only as precise as its cleaning, curing, and finishing steps, and the best systems include or integrate with automated post-processing to remove variables that cause dimensional shifts. Ultimately, the top manufacturers worth considering combine robust hardware, honest material support, and software that keeps the machine true, rather than chasing spec-sheet numbers alone.
Contact Us
Contact Person: Joe
Email: [email protected]
Tel/WhatsApp: +8613799507208
Website: https://www.3dprotomat.com/