OEM Open Type Fiber Laser Cutting Machine: The Ultimate Guide to Precision and Efficiency
2026-10-10
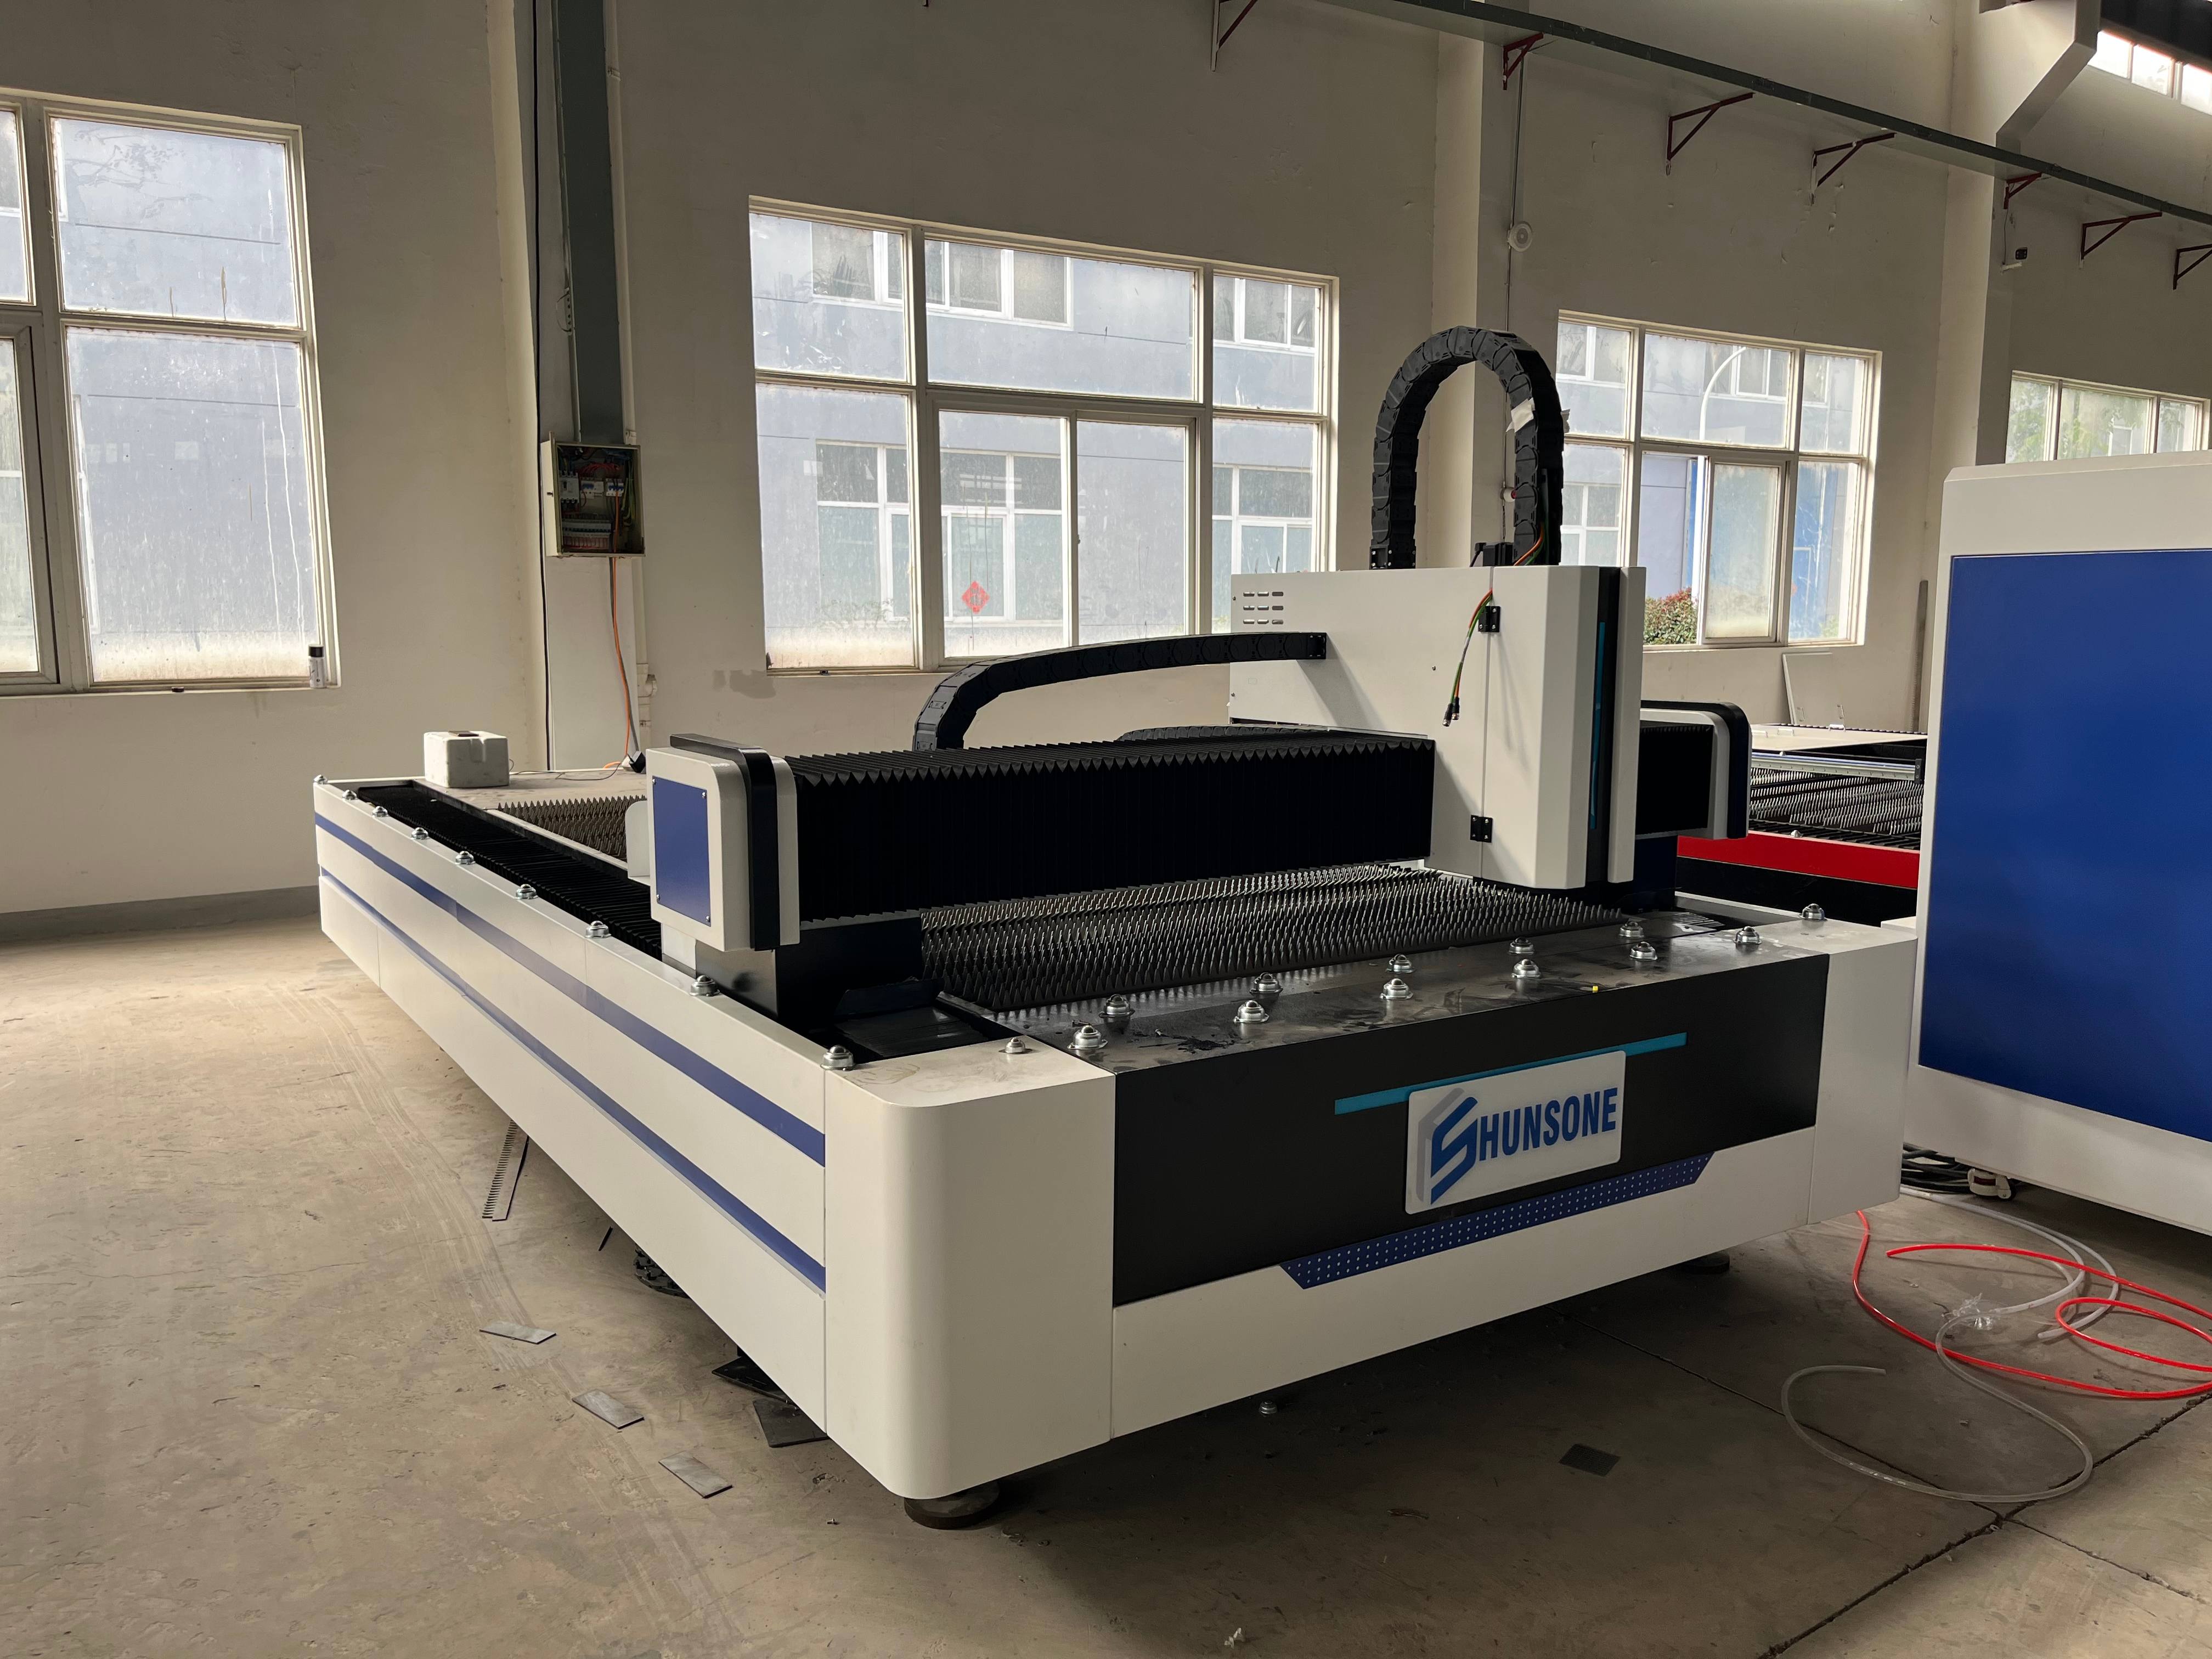
If you’ve ever watched a fiber laser slice through steel like butter, you know precision isn’t just a spec sheet promise—it’s the difference between scrap and a perfect fit. But what happens when you need that same cutting power in an open, modular setup that adapts to your production line, not the other way around? That’s where OEM open type fiber laser cutting machines enter the picture, and HUNSONE has been quietly refining this category for years. In this guide, we’ll walk you through exactly how open type designs boost both accuracy and throughput, what to look for in an OEM partner, and why the right machine can turn your cutting department into a profit center instead of a bottleneck.
What an Open Type Frame Changes on the Shop Floor
An open type frame alters how operators move around the machine. The open front and sides let a forklift drop a die stack directly into the work area without threading it through a narrow throat. You stop reserving half the shift for awkward crane angles and start using that time for actual forming work.
Tool changes become less of a chore because the die space is visible from three directions. A setup person can see the alignment marks without crouching under a beam or using a mirror. When a part sticks, reaching in from the side takes seconds instead of calling for a pry bar and a second pair of hands.
Maintenance also shifts. With the frame open, you can inspect the ram guides and gibs without pulling the upper structure apart. That changes the preventive maintenance schedule; tasks that used to require a full teardown now happen during a lunch break. The floor itself feels less like a corridor around a machine and more like a working zone around a tool.
Where Fiber Laser Precision Actually Comes From
Precision in a fiber laser doesn't appear out of thin air, and it's not just a matter of cranking up the power or using a fancier lens. The real source sits deep in the architecture of the laser itself: a doped optical fiber that behaves as the gain medium. Because light is generated and amplified inside a hair-thin core, the beam emerges with a near-perfect spatial mode and remarkably stable pointing. There are no bulky mirrors to drift out of alignment, no gas tubes that shift with temperature. That inherent stability is the quiet foundation everything else builds on.
From there, precision gets shaped by the control electronics. A fiber laser can fire pulses on a timescale measured in nanoseconds or even femtoseconds, and the driver board decides exactly how many joules land in each pulse, how fast they repeat, and how the beam ramps up and down. This isn't just on-off switching; it's fine-grained modulation that lets the same machine cut foil-thin shim stock or engrave a hardened tool surface. Combine that with a galvo scanning head that positions the beam to within microns, and you get repeatability that thermal or mechanical drift would ruin in older laser types.
Even the delivery fiber matters more than people expect. The beam doesn't travel through open air where dust, humidity, or slight misalignment can scatter it. Instead, it stays inside a protected glass waveguide all the way to the focusing head. That means the spot size at the workpiece stays consistent hour after hour, and the process doesn't need constant re-zeroing like lamp-pumped or CO2 systems. So when you see a fiber laser cutting a contour with edge quality that looks ground, remember it's not one clever trick—it's an entire chain of design choices, from doped core to scan head, each keeping its own piece of the error budget tiny.
Dialing In Cut Quality Across Different Metals and Thicknesses
Getting a clean cut on thin stainless steel demands a different rhythm than slicing through thick aluminum plate. Most operators learn this the hard way after watching a perfectly good edge turn ragged because they trusted one generic setting. The real trick is recognizing that each metal carries its own thermal personality: steel holds heat and resists the cut, aluminum sheds it so fast the kerf wants to close up, and copper laughs at your assumptions entirely. Instead of chasing some mythical universal parameter, start by mapping how the arc behaves at 16 gauge versus half-inch stock. On thin sheet, reduce amperage just enough to keep the puddle moving without blowing out the back side; on thick sections, push more heat but slow the travel speed so the beam actually penetrates instead of skating across the surface.
Thickness changes everything about gas pressure and nozzle standoff, which is where a lot of folks get stuck. With mild steel under a quarter inch, you can run fairly tight focus and moderate assist gas, but jump to three-quarter plate and suddenly you need a wider kerf to let molten metal evacuate cleanly. A simple habit that pays off: before each job, scribble the material type and thickness on the machine's setup sheet, then adjust the focal point in or out by a millimeter or two and watch the spark spray pattern. If the sparks angle back toward the nozzle, the cut is lagging and you need more speed or less material; if they spray straight down and the dross wipes off with a glove, you're dialed. No chart beats that kind of immediate feedback.
Of course, edges are only half the battle—heat-affected zones and warping sneak in quietly on thicker sections. One practical move is to sequence your cuts so the part cools unevenly on purpose, or use a short pierce delay on stainless to avoid work-hardening at the start point. For aluminum beyond three-eighths, consider switching from nitrogen to a helium-argon mix if your setup allows; it stabilizes the arc in a way pure argon can't manage at high current. The goal isn't perfection on the first try, but building a mental library of what “right” sounds like—the hiss of a proper cut versus the sputter of a struggling one. Once you can hear that difference, the settings stop being numbers and start being a conversation with the metal.
Keeping Dust and Heat from Sabotaging Your Uptime
Most downtime never starts with a dramatic failure. It begins with a thin layer of dust settling on fan blades, heat sinks, and intake vents. That layer insulates components, slows air movement, and pushes internal temperatures higher than design limits. Over time, capacitors dry out, solder joints stress, and power supplies run less efficiently. A monthly visual check of air filters, combined with a schedule for replacing or cleaning them, is far cheaper than an emergency swap at 3 a.m.
Heat has a sneakier pattern. Even if the room feels cool, hotspots can form behind racks or along cable bundles that disrupt airflow. Intake and exhaust separation matters more than total cooling capacity. Check temperature sensors at the top of every rack, not just at the thermostat. If a single cabinet runs 8 to 10 degrees hotter than the others, treat it as a warning sign. Rearranging blanking panels and sealing unmanaged cable openings often drops temperatures more than adding another CRAC unit.
Pair dust control and thermal monitoring into one weekly routine. While checking filters, glance at fan speeds and error logs for any device throttling its CPU. Small changes compound quickly. A clean, cool system does not just run longer; it also buys you time to schedule maintenance during normal hours instead of reacting to a total outage.
How OEM Open Type Builds Give You More Control
Many preloaded system images lock you into a fixed set of features, but OEM open type builds flip that relationship. Instead of accepting whatever the manufacturer decided to include, you can modify core components, strip out unwanted modules, and integrate your own utilities. This flexibility means your device starts acting like a platform you shape, not a closed box you merely operate.
The real advantage shows up in how you handle updates and patches. With an open type build, you can apply your own security fixes or roll back a problematic library without waiting for a vendor's quarterly release cycle. That kind of direct access reduces downtime and lets you align the software with your operational needs, whether you're managing a single device or a fleet.
Configuration also becomes less about digging through hidden menus and more about editing a clear set of build parameters. You can turn off telemetry, enable experimental drivers, or rebuild a system image with only the libraries you actually use. Because the build process is transparent, every change is traceable, and you're never left guessing which process is consuming resources or phoning home.
Setting Up the Machine for Repeatable Day-to-Day Output
A machine that produces reliable day-to-day output is not the result of a single grand adjustment, but of a quiet alignment between expectation and reality. It begins with understanding the tolerance stack across every moving part: the slight drift in bearing preload after a thermal cycle, the variation in lubrication viscosity overnight, the way a worn belt settles into a slightly different neutral position. Rather than chasing perfect zeros on the dials, a seasoned operator maps how these small drifts interact, then locks in compensation points that hold the output within a comfortable band. The machine never stays perfectly still, but it learns to repeat its own personality.
Repeatability also demands that the environment around the machine stops being a variable. A draft from an open bay door, a shift in floor leveling after rain, or the subtle difference between the morning and afternoon shop temperature can all push output beyond the acceptable window. Sealing off these external influences—thermal curtains, isolation pads, or simply a consistent daily startup sequence—matters more than any bolt-by-bolt spec. The goal is to give the machine a familiar stage on which to perform, so that day after day, the first part off the line lands within the same narrow range as the last part yesterday.
Finally, the operator’s routine becomes part of the machine’s repeatability. The order of cleaning, the torque used on each fixture clamp, the exact height at which the tool is set before the first cut—these small habits are not just preferences; they are inputs to the output. Writing them down in a simple checklist, then following that list without improvisation, turns a good setup into a repeatable one. When the machine is finally set up for consistent daily output, the proof is not in the settings themselves, but in the absence of drama: parts come out the same, hour after hour, without anyone needing to hover or correct.
FAQ
An OEM open type machine is built on a gantry-style frame without the full protective cabin seen on enclosed units. That openness lets operators load oversized or heavy sheets from the top or side using an overhead crane or forklift, which is a huge advantage in job shops that handle thick plate. The OEM aspect means the manufacturer can brand the machine to your specifications and adjust components like the laser source, cutting head, and control system. Enclosed models prioritize containment and fume control, while open types trade some built-in safety for easier material handling and lower initial cost.
Fiber laser sources excel on reflective metals that often give CO2 lasers trouble. You can cut stainless steel, carbon steel, aluminum, brass, and copper cleanly. Thickness capacity scales with laser power: a 1kW source typically handles carbon steel up to 10mm and stainless or aluminum up to 5mm, while a 6kW unit can push through 25mm carbon steel and 16mm aluminum. Always match the lens and assist gas to the material; oxygen speeds up mild steel cutting, nitrogen yields oxide-free edges on stainless.
Fiber lasers emit at roughly 1.07 microns, about one-tenth the wavelength of CO2. This shorter wavelength focuses to a much smaller spot, producing a narrower kerf and tighter tolerances—often within ±0.05mm on thin sheet. The beam also has better mode quality, so the energy density stays high through the cut, reducing thermal distortion. For intricate contours and fine features, fiber simply holds the line better, and the minimal heat-affected zone keeps edges sharp without heavy post-processing.
Efficiency shines when you're moving big plates constantly. Without walls in the way, an operator can load a 3m×1.5m sheet in under a minute using a crane or vacuum lifter, while an enclosed machine would need the front door opened and material slid in. Open frames also simplify multi-station workflows because you can access the cutting area from three sides for setup, part removal, or quick nozzle changes. For a job shop running small batches of varied parts, that access reduces non-cutting time dramatically.
Yes, the lack of an enclosed cabin means you need a dedicated laser safety zone. Standard practice is to fence the machine with interlocked perimeter guarding and light curtains that stop the beam if someone enters. Operators wear certified laser goggles matched to the fiber wavelength. Fume extraction remains critical—an open design benefits from a downdraft table or overhead hood to capture metal dust and vapors. With proper enclosures, warning signs, and lockout procedures, an open type machine meets the same safety standards as enclosed alternatives.
Start with the laser source and cutting head—brands like IPG, Raycus, and MAX have different reliability and service networks. Check the frame’s stress-relieved welded steel construction and the rack-and-pinion or ballscrew drives; those determine long-term accuracy. The control system matters too: CypCut or Beckhoff interfaces are user-friendly and support common CAD files. Since it's OEM, clarify customization depth—can you choose the paint color, logo placement, and component specs? Also confirm local technical support and spare parts availability, because downtime on an open bed stops production just as fast as on an enclosed one.
Fiber laser sources are nearly maintenance-free compared to CO2 tubes, but the motion system and optics still need routine care. Daily, wipe the protective window and check the nozzle for spatter. Weekly, clean or replace the air filters and inspect the lens for pitting. Monthly, grease the rails and pinions, drain moisture from the air system, and verify the chiller coolant level. The cutting head’s ceramic ring and focus lens have finite lives, so keep spares on hand. A disciplined 10-minute daily routine prevents most unscheduled stops.
Absolutely. The open gantry design works well with automated loading and unloading systems, whether it's a shuttle table, robotic arm, or conveyor-based sheet storage. Many OEM builders offer integration kits with Ethernet/IP or Profinet connectivity so the laser cell reports status and accepts job queues from a central MES. Because the bed is accessible from the top, a gantry crane can drop sheets directly onto the slats, then a parts-picking robot can retrieve finished pieces from the skeleton. This flexibility makes open type machines a favorite for lights-out manufacturing setups.
Conclusion
An open type frame changes how a shop floor works in ways that go beyond just saving space. With no full enclosure in the way, operators can load large or awkward sheets without fighting the machine, and routine cleaning or nozzle checks happen in seconds instead of minutes. At the same time, fiber laser precision is not a single magic setting. It comes from how the resonator, cutting head, and motion system stay in sync. Dialing in cut quality across mild steel, stainless, aluminum, or brass means adjusting focal position, gas pressure, and feed rate together rather than chasing one number on a screen. Small changes to assist gas or nozzle standoff often make more difference than a higher wattage ever will.
Keeping dust and heat from eating into uptime is where many shops trip. Open builds make this easier because you can see buildup before it becomes a problem, but that only helps if extraction and cooling are sized correctly for the work you actually run. OEM open type machines give you more control here—not just in the software, but in choosing the chiller, filtration, and table design that fit your parts and your shift pattern. Once that foundation is set, repeatable day-to-day output comes down to simple discipline: clean the lens on a schedule, check nozzle centering after every material change, and keep a written log of settings that already worked. That kind of consistency, more than any single feature, is what turns precision and efficiency from a brochure phrase into a daily result.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/