Sliding DU Bushing Maker Guide for Superior Performance
2026-11-16
In precision engineering, sliding DU bushings are the unsung heroes that keep assemblies moving smoothly under load. Yet not all manufacturers deliver the same level of durability and low-friction performance. This guide explores the key factors behind a superior DU bushing maker—from material selection to surface treatment—and highlights why XIAYI has become a trusted name for applications where failure is not an option.
Material Selection for Wear Resistance Beyond Standard Specs
Standard material specs often fall short when wear involves combined mechanisms—say, abrasion plus impact or corrosion-assisted erosion. Instead of defaulting to a generic high-hardness alloy, experienced engineers map the contact stress, particle size, and chemical environment first. For sliding wear under low impact, a cast cobalt-chromium overlay may outperform a harder but brittle tungsten carbide cladding, simply because the matrix can absorb micro-deformation without cracking.
Beyond conventional steels and hardfacing, ceramic-metal composites like silicon carbide–reinforced aluminum or zirconia-toughened alumina offer targeted resistance in high-temperature or acidic conditions. These choices rarely appear in baseline specs, yet they prevent the frequent replacement cycles that inflate lifecycle costs. The key is to test candidate materials under the actual wear mode—ASTM G65 dry sand abrasion or ASTM G77 block-on-ring—rather than relying on a single hardness number.
Another overlooked path is tailoring surface treatments after machining. Nitriding, boriding, or diamond-like carbon coatings can push a standard 4140 shaft well beyond its catalog rating without a costly alloy upgrade. Pairing the right treatment with a base material that has sufficient core toughness yields a wear system that standard material selection charts miss.
Sintering Practices That Avoid Brittle Bronze Layers
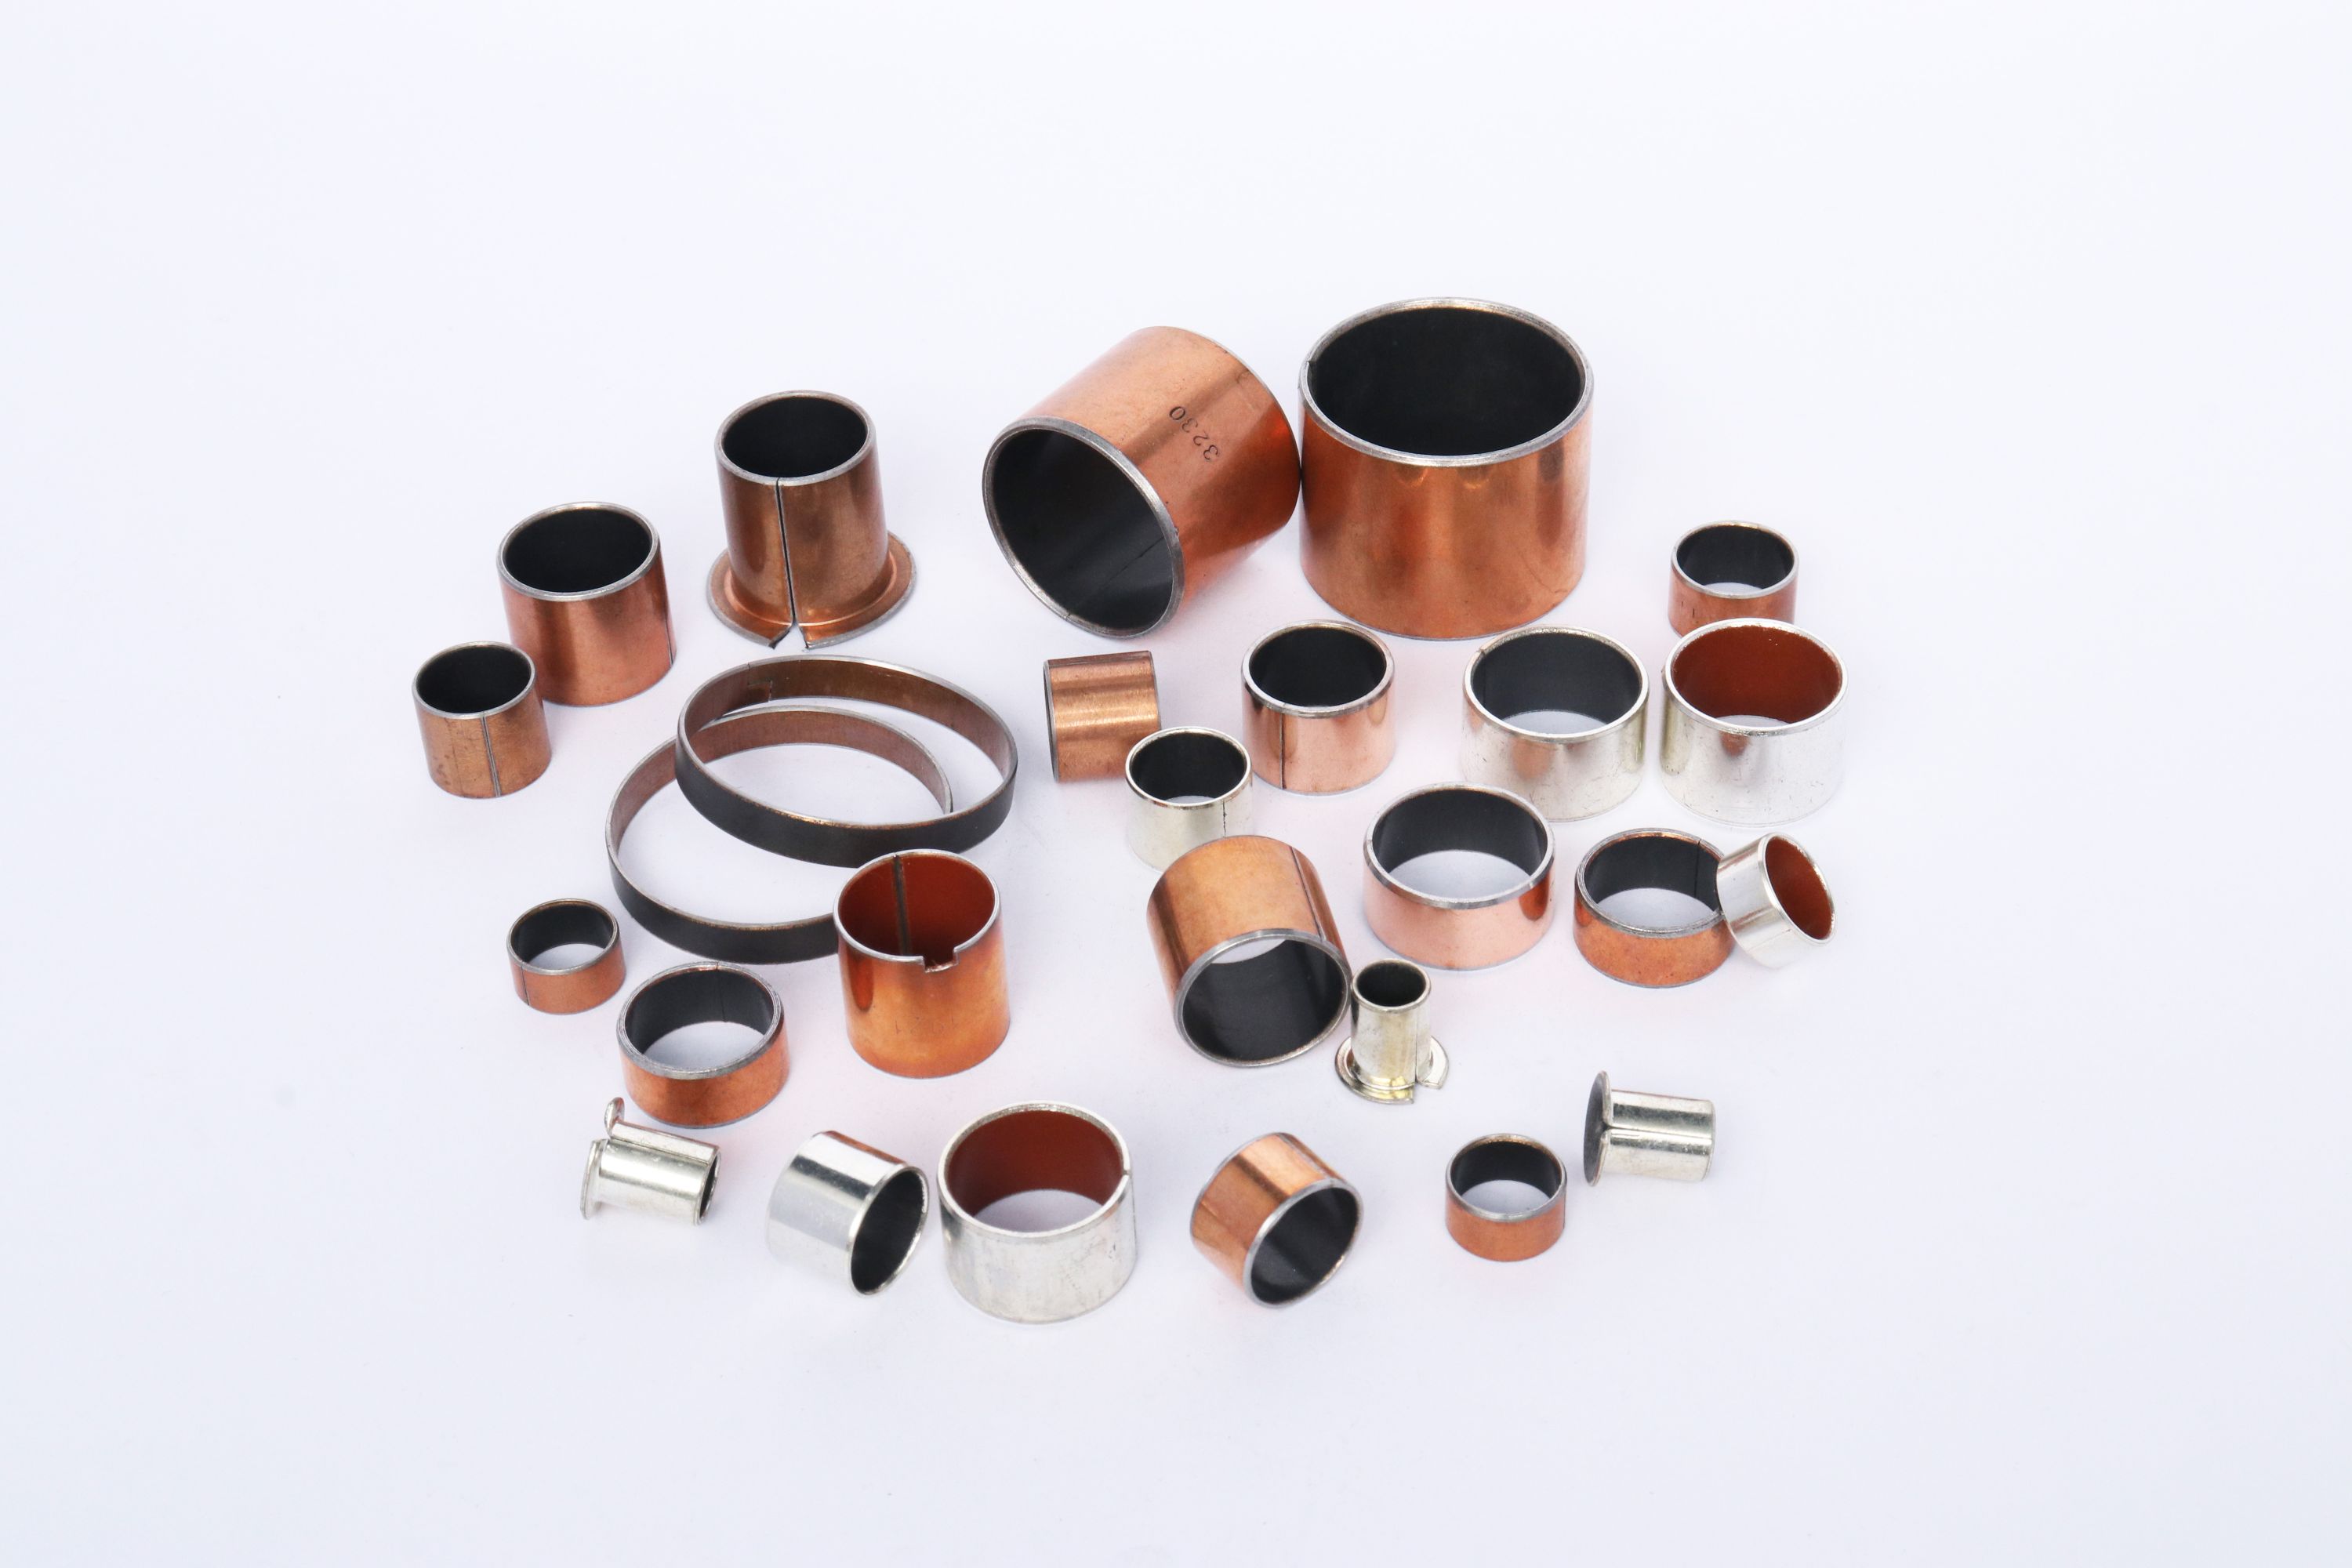
Brittle bronze layers often show up when tin-rich phases segregate near grain boundaries during uneven heating. If the compact passes through the alpha-to-beta transition too quickly, diffusion can’t keep up, leaving behind hard intermetallic islands that crack under load. Instead of ramping straight to peak temperature, a stepped schedule with a hold around 800–820°C gives the tin time to migrate evenly. This simple change reduces the sharp hardness gradient that turns a tough bronze part into a fracture-prone one.
Atmosphere control matters more than most shops admit. Traces of oxygen or moisture create tin oxide films along particle contacts, and those films act as crack nucleation sites. A dry hydrogen or dissociated ammonia atmosphere with a dew point below -40°C strips away surface oxides without decarburizing the alloy. Some operators add a small amount of phosphorus-bearing master alloy—around 0.1% by weight—to tie up residual oxygen before it can embrittle the interparticle necks.
Cooling after sintering is where many batches go wrong. Quenching from the sintering zone may look efficient, but it traps thermal stresses and promotes formation of a continuous brittle delta phase network. A controlled cooling rate of 5–10°C per minute through the 500–300°C range lets the structure relax into a more ductile alpha-plus-delta mixture. If the part has thick and thin sections, consider a brief soak at 600°C before final cooldown to even out internal temperature differences.
Impregnating PTFE Without Blocking Pores
Keeping pores open while impregnating PTFE rarely succeeds by simply dipping the membrane in a bath. The impregnant's viscosity and surface tension dictate whether it coats the fibril network or fills the voids. Diluting the impregnant in a volatile solvent drops both, so the liquid moves through the pores as a thin film rather than a plug. A gentle vacuum helps pull the diluted mixture through, leaving only a light deposit on the pore walls after the solvent flashes off. The result keeps airflow intact.
A sacrificial filler can also reserve the pore volume. Saturate the PTFE with a low-boiling liquid that doesn't mix with the impregnant, then treat the surface or edges. The impregnant remains at the exterior and near the pore mouths because the inside is already occupied. Once heat removes the filler, the original open channels reappear. This trick works for high-viscosity impregnants that would otherwise lock the structure solid.
For heavier loadings, short vacuum cycling offers more control. Pull a moderate vacuum to evacuate air from the pores, then introduce the impregnant and release the vacuum. The pressure change drives material into the small spaces, but the cycle should be stopped before the liquid coalesces and cures into a continuous blockage. Checking air permeability between cycles tells you if you have pushed too far.
Machining Tolerances That Prevent Binding Under Load
When two mating parts experience load, the clearance that seemed adequate on the drawing can vanish instantly. A classic oversight is using a standard running fit like H7/g6 for a shaft that deflects under a radial force. The shaft bows, and the bore's effective entry angle changes, causing edge contact that digs in like a wedge. To avoid this, calculate the maximum elastic deformation of each component under the worst-case load, then add that deflection value to the minimum diametral clearance. For a simply supported shaft, deflection at the midpoint can be approximated with beam formulas; this number isn't a suggestion—it's the floor for your clearance budget.
Thermal expansion often plays the villain too. A stainless steel pin inside an aluminum housing will tighten as temperature rises because aluminum expands roughly twice as much as stainless. If the assembly runs hot, the room-temperature clearance must account for the differential growth. Compute the change in diameter for each material using the coefficient of linear expansion and the operating temperature range, then subtract the smaller growth from the larger. That differential reduces your effective clearance, so the initial fit must be looser than a room-temperature-only design. Skimping here leads to a bound joint that can only be freed with a hammer.
Surface texture and geometric errors are the silent killers of sliding fits. A turned surface with a roughness average of 3.2 µm Ra still has peaks that can plastically deform under load, reducing the effective gap. Specifying a controlled waviness and cylindricity—not just size tolerance—keeps the contact patch from concentrating at one end. For shafts over 100 mm long, add a straightness or total runout tolerance of 0.01 mm per 100 mm of length to prevent the banana effect. The mating bore should carry a matching cylindricity, otherwise the two imperfect forms interlock under load instead of gliding. When in doubt, run a tolerance stack-up that includes form errors, surface peaks, deflection, and thermal expansion; if the total available clearance doesn't clear that stack, binding is not a matter of if, but when.
Break-In Procedures That Reduce Early Scoring
Freshly machined bores and rings start with microscopic peaks that can concentrate heat and pressure. A careful break-in routine keeps the oil film intact while letting those surfaces mate gradually. Instead of idling or holding a steady speed, use short bursts of moderate acceleration followed by engine braking to seat the rings without polishing the bore.
Avoid lugging the engine during the first few hundred miles. Low rpm with heavy throttle pushes the piston hard against the cylinder wall with poor oil splash, which is a common trigger for early scoring. Choosing a break-in oil with enough zinc and phosphorus also gives the cam and cylinder surfaces a protective buffer until clearances stabilize.
Field Inspection Routines for Predicting Replacement Cycles
Field inspection routines rarely follow a rigid schedule when you're trying to anticipate replacement cycles. A better approach is to walk the site with a simple checklist that prioritizes visible wear, corrosion, and unusual vibration or heat patterns. Instead of waiting for a quarterly audit, many maintenance teams now pair routine walkthroughs with small, handheld tools—thermal cameras, thickness gauges, or even a basic feeler gauge—to catch early signs of degradation before they show up in performance data.
The real value comes from turning those field notes into a rolling forecast. For example, if a pump bearing shows slight pitting during two consecutive inspections, you can estimate the remaining service life based on load history and environmental exposure. That shifts the conversation from "when did we last replace it?" to "how fast is it wearing under current conditions?" Over time, these observations build a local database of failure patterns that no off-the-shelf manual can replicate.
One overlooked aspect is training inspectors to record what they see, not what they expect. A rust streak near a flange, a faint harmonic from a fan housing, or a slight misalignment in a belt guard—these small details often get dismissed as cosmetic. But when logged consistently, they form the earliest signals of a component approaching the end of its useful life. Pair those logs with simple trend charts, and you'll find replacement cycles emerging naturally from the field, rather than being forced by a calendar.
FAQ
DU bushings use a steel backing, a porous bronze sinter layer, and a PTFE-lead overlay, so they run dry and handle higher loads without external lubrication.
Request sample batches, ask for ISO 9001 or IATF 16949 certifications, check their tolerance control on the ID after swaging, and look at how they bond the PTFE layer to the bronze.
Focus on maximum dynamic load, PV limit, operating temperature range, and wear rate at your specific speed. Don't just chase the lowest coefficient of friction.
Yes, but you need to confirm the backing material and edge treatment. Standard steel backs can rust, so many makers offer stainless steel or coated versions for washdown areas.
Use hardened steel or stainless shafts with a ground finish around Ra 0.2–0.4 µm. Avoid soft shafts because they accelerate wear on the PTFE overlay.
Misalignment, edge loading, or a shaft finish that is too rough often causes premature wear. Also, if the housing bore is out of round, the bushing can't keep its proper running clearance.
Dimensional checks for ID, OD, and wall thickness, material certificates for the steel and bronze layers, overlay thickness measurements, and PV test data or wear test results under your operating conditions.
There is a short running-in phase where the PTFE transfer film forms on the shaft. Start with lighter loads and lower speeds for the first few hours, then gradually move to full duty.
Conclusion
A sliding DU bushing only performs as well as the decisions made long before it reaches the press fit. Start with the bronze layer: rather than chasing a single hardness number, look for powders that balance embedded graphite pockets against a tough, work-hardening matrix. Standard specs often accept brittle sintered skins that crack under edge loading, so the better route is to adjust sintering temperature and time so the bronze fuses deeply without becoming glass-hard. Then move to PTFE impregnation. The goal is not to fill every void but to leave a controlled network of open pores that hold oil while the PTFE-rich surface carries the initial movement. Machining tolerances matter just as much; a bore that is too tight will pinch the bushing and wipe the lubrication film before it forms, while too loose a fit lets the bushing walk and fret against the housing.
Break-in is where many otherwise sound bushings fail early. Run the first few hundred cycles under reduced load and keep speeds moderate, which lets transferred PTFE form a smooth glaze instead of tearing away as debris. Watch for the first signs of scoring, not by waiting for noise, but by checking surface temperature and oil discoloration after short intervals. In the field, replace inspection routines based on calendar hours with measurements of wear depth at two or three points around the bushing’s loaded zone. A sudden increase in clearance often predicts failure long before seizure, and combining that trend with vibration or shaft play data gives a practical replacement trigger. The guide’s core idea is simple: superior performance comes from matching each step to the actual load and movement, not from copying a generic bushing recipe.
Contact Us
Contact Person: Leela
Email: [email protected]
Tel/WhatsApp: 8613586885132
Website: https://www.xiayishockparts.com