Stainless Steel Flat Washers Factory Production Secrets Revealed
2026-09-26
Ever wondered what really goes on inside a stainless steel flat washer factory? Most buyers assume it's just stamping metal—until they see the rejects pile up. At Wanluo, we've spent years refining processes that most suppliers keep hidden. In this post, we're pulling back the curtain on the production secrets that separate a washer that lasts from one that fails.
First Shift: What Happens Before the Presses Start
The print floor at 5:40 a.m. is a quiet beast. Fluorescent tubes flicker to life one by one, casting pale light over the hulking offset presses that stand silent and waiting. A few early-shift operators move through the space with the kind of unhurried precision you only get from years of repetition. Someone drags a pallet jack stacked with paper into position near the feeder; another kneels to inspect the blanket cylinder with a flashlight, running a gloved finger over the rubber surface. The air still smells faintly of solvent from the night cleanup, mixed now with coffee from a thermos left on a workbench.
Before anything spins, the press crew walks through a checklist that never gets shorter. Ink trays are filled by hand, each color matched against a swatch taped to the console—magenta slightly warmed, cyan pushed a touch darker than the proof. Plates are bent and locked onto the cylinders, their registration marks aligned under a magnifier. A lead operator crouches at the dampening system, adjusting the water feed until the rollers glisten evenly without dripping. Nobody says much. The work is in the fingertips and the feel of a knob turned a quarter degree too far, then eased back.
The last ten minutes before the run are always the same: a single slow revolution of the press by hand, enough to pull paper through and expose any hidden flaw. The crew gathers around the delivery end, watching the first sheets drop onto the pile. One person checks the ink density against a color bar; another folds a sheet in half to verify the dot gain. If something's off, the press stays silent while adjustments are made. Only when the lead operator nods—once, to no one in particular—does the motor hum climb to running speed, and the real noise of the day begins.
The 0.02 mm Flatness Gap That Dooms a Washer
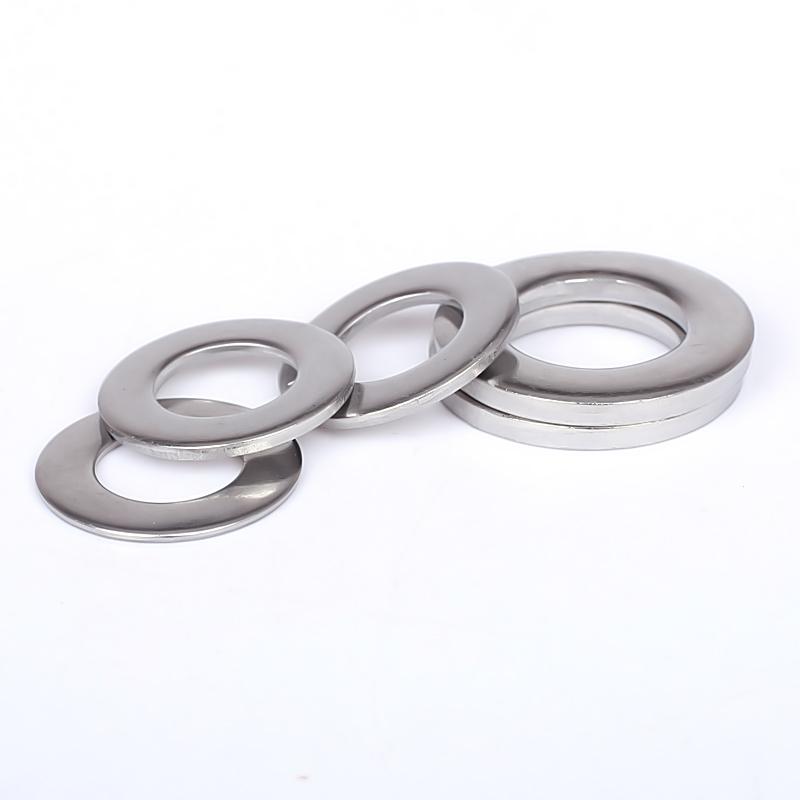
A washer's job seems simple: sit flat, spread load, keep things tight. But the moment its surface deviates by as little as 0.02 mm from true flatness, that job quietly falls apart. Under enough clamping force, the tiny gap becomes a stress riser. The high side digs in, the low side floats, and the bolt sees uneven tension. What starts as a cosmetic imperfection ends as a fatigue crack waiting to open.
The reason this seemingly trivial offset matters has to do with how washers bridge surface irregularities. In a perfect setup, the washer makes full contact with both the nut and the substrate. With a 0.02 mm variation, that contact breaks into a few concentrated patches. These patches carry all the load, often exceeding local yield strength. Over repeated thermal cycles or vibration, the material creeps, the gap widens, and preload disappears. The joint loosens without anyone noticing a visible fault.
Engineers sometimes dismiss such small numbers, but failures in bolted connections rarely announce themselves with big deformations. The 0.02 mm gap works like a slow leak. It lets micro-motion begin at the interface, accelerates fretting, and invites corrosion into the crevice. Once that starts, the washer is no longer protecting the joint — it's actively compromising it. Flatness isn't a luxury spec here; it's the entire reason the part exists.
Why the Edge Burr Tells You Everything
A burr on a machined edge is not just leftover material you file off and forget. It is a physical record of the entire cutting event, captured in metal. The size, shape, and direction of a burr reveal how the tool entered the cut, how sharp or dull it was, and whether the feed and speed matched the material. Once you learn to read this tiny ridge, you stop guessing about your process and start seeing exactly what happened at the point of contact.
Take two burrs that look almost identical at a glance. One is thin and curls away cleanly, breaking off with light finger pressure. That usually means the tool was sharp and the chip flowed smoothly. The other burr is thick, jagged, and folded back against the surface. That points to a worn edge, excessive feed force, or poor chip evacuation. Even the direction of the burr tells you which way the material was pushed, and whether the geometry of the tool matched the job.
What makes the edge burr so valuable is that it never lies. Surface finish can be polished later, and dimensions can be corrected, but the burr forms in real time as the tool and workpiece fight each other. It is the most honest witness to the cut. Watching how a burr changes from part to part helps you catch a dulling insert or a drifting parameter long before it shows up as scrap. Ignore the burr, and you are throwing away the most direct feedback the process will ever give you.
Inside the Annealing Furnace: Where Stress Gets Erased
Walk past an annealing furnace mid-cycle and you won’t hear much—no hammering, no quenching hiss, no visible glow in some low-temperature runs. What’s happening inside is a slow-motion rearrangement of the metal’s crystal lattice. Cold working had shoved atoms into positions they wouldn’t choose on their own, and the heat gives them just enough mobility to find less strained arrangements.
Temperature alone isn’t the whole story. The holding time at peak heat matters because it allows the entire load, including the thickest sections, to catch up. Then the cooling curve takes over. Drop the temperature too fast and the surface contracts while the core is still expanding, which creates a whole new set of residual stresses before the parts even leave the furnace. A slow, even ramp down is what keeps the relief from turning into a new problem.
The real skill is reading the batch, not just the setpoint. Thermocouples placed at different points can tell you if one corner of the furnace lags behind. Skilled operators adjust the burners or elements to keep the heat front moving evenly. In the end, the furnace doesn’t force stress out—it simply creates conditions where stress no longer has a reason to stay.
The Sorting Room’s Silent Quality War
Every morning, the sorting room hums with the same fluorescent buzz, but beneath it runs a quieter contest. No one announces the rules, and no scoreboard hangs on the wall. Instead, the evidence shows up in small ways: a mislabeled bin corrected before the shift lead notices, a stack of returns re-folded with sharper corners, a batch of mixed inventory separated without being asked. The veterans call it pride. The newcomers call it pressure. Most just keep their heads down and let their hands argue.
The real battle isn't against quotas or clock-outs, though those shadow every move. It's about noticing the things that never make it into a report. A torn sleeve gets taped instead of tossed. A stray barcode gets matched to the right shelf. Someone quietly reworks a cart that was already marked done. These small acts pile up until the room develops its own unspoken standard, and falling below it feels worse than a formal write-up.
Final Inspection: The Five-Second Test That Cuts Returns
Before sealing the box, pause for five seconds. Scan the item the way a tired, slightly skeptical customer would. Is the stitching straight? Does the color match the photos? Would you be disappointed if this landed on your doorstep tomorrow morning? That quick gut check catches the loose thread, the smudged lens, the missing instruction card before they become reasons for a refund.
Most returns aren't from catastrophic failures. They come from small mismatches between expectation and reality. The five-second test forces you to see the product fresh, not as the person who made or packed it. Run your thumb along the edge. Flip it over. Open the clasp. If anything snags your attention, fix it now or pull the item. A few seconds at the packing bench saves a week of back-and-forth and a disappointed customer.
Make the check a habit, not a chore. Keep a short mental list: smell, symmetry, function, finish. You'll catch defects early, and your return rate will drop without adding headcount or expensive software. It's the cheapest quality control you'll ever run.
FAQ
Running overnight lets them avoid peak electricity rates and keeps the stamping dies at a stable temperature, which reduces dimensional drift in thin washers.
Many shops use a slight taper on the punch and increase the die clearance just enough to shear cleanly. A secondary tumbling step with ceramic media knocks off any micro-burrs without rounding the edges too much.
It usually comes down to the customer's exposure to chlorides. 304 handles general moisture, but if the washers sit near saltwater or chemical washdowns, 316's molybdenum content prevents pitting.
Yes, some lines use a double-action press that blanks and forms in one stroke, while an in-die sensor measures thickness every few cycles and adjusts the feed automatically.
The leftover stainless steel lattice is baled and sold back to mills for remelting. Factories track the scrap weight against raw material input to catch tool wear or hidden yield loss.
Passivation removes free iron particles left from tooling contact. Without it, those tiny particles can rust and leave brown spots on the washer surface, making a good product look defective.
Tooling upkeep. A worn punch or die can still make a washer that looks fine but has a slightly undersized hole or a ragged edge. High-volume factories rotate dies for sharpening far more often than outsiders expect.
Conclusion
Before a single press cycles on the morning shift, the operator already knows which coils will fight back. They run a micrometer across the raw strip, checking thickness at three points, and flex a sample by hand to feel for hidden lamination. The tolerance everyone fears is flatness: 0.02 mm of crown or wave means the washer will rock on a mating surface and never clamp evenly. That is why the blanking die gets a stone-dressing before first hits, not after. Once stamping starts, the edge burr becomes the loudest signal. A burr that rolls over instead of snapping off means the die clearance is shifting, and if left alone, it will tear the next thousand pieces. After blanking, washers go into the annealing furnace at roughly 1,050°C, where the metal recrystallizes and stamping stress is erased. Without this soak, the washer would spring back unpredictably and crack under torque.
The sorting room is not quiet in the sense of low volume—it is quiet because every hand is listening. Experienced sorters drop each washer onto a granite plate; a dull thud means a hidden crack, while a clean ping passes. They also roll washers down a slight incline to catch any out-of-round condition that a gauge might miss. Final inspection is where the five-second test lives: a worker picks up a washer, runs a thumbnail around the edge to feel for burr, lays it on a flat glass surface and slides a 0.02 mm feeler under it, then hits it with a small magnet. If the magnet sticks too hard or the feeler slips through, the batch gets quarantined. That five seconds has cut returns to nearly zero, not because the test is fancy, but because it catches exactly what customers hate—a washer that looks fine but fails on the line.
Contact Us
Contact Person: Shane
Email: [email protected]
Tel/WhatsApp: 8613357785029
Website: https://www.wanluohardware.com