Ultrasonic Spray Pyrolysis System Manufacturer Delivers Precision Thin-Film Coating Solutions
2026-10-23
Thin-film coating precision has never been more critical, and one manufacturer is quietly setting a new standard. Siansonic, known for its ultrasonic spray pyrolysis systems, delivers uniform coatings that others struggle to match. What makes their approach different? Dive into the technology behind the name at Siansonic and discover why industry leaders are paying attention.
The Role of Ultrasonic Nozzles in Film Uniformity
Most spray nozzles rely on hydraulic pressure to shove liquid through a tiny orifice, which naturally produces a wide range of droplet sizes and a pulsing flow that shows up as streaks or mottling on the substrate. Ultrasonic nozzles take a different route. They vibrate a titanium tip at frequencies above 20 kHz, and the liquid simply rides along the surface, breaking into droplets at the atomization edge. Because the vibration is constant and the liquid feed can be extremely low, you get a nearly monodisperse spray with no pressure surges. That steadiness matters enormously when you are laying down a film only a few microns thick—any hiccup in flow becomes a visible defect.
Another factor often overlooked is how ultrasonic energy prevents the nozzle from clogging mid-run. A conventional air-atomizing nozzle might start out fine, but as solvent evaporates near the tip, solids accumulate and alter the spray pattern, dragging down film uniformity across the batch. The ultrasonic tip keeps vibrating, so particles cannot easily adhere. This self-cleaning behavior means the droplet size distribution stays consistent from the first wafer to the last, even with suspensions or high-viscosity polymer solutions. The result is a film with the same thickness and optical clarity at the edges as in the center, without needing constant operator intervention.
Adjusting Spray Parameters for Repeatable Results
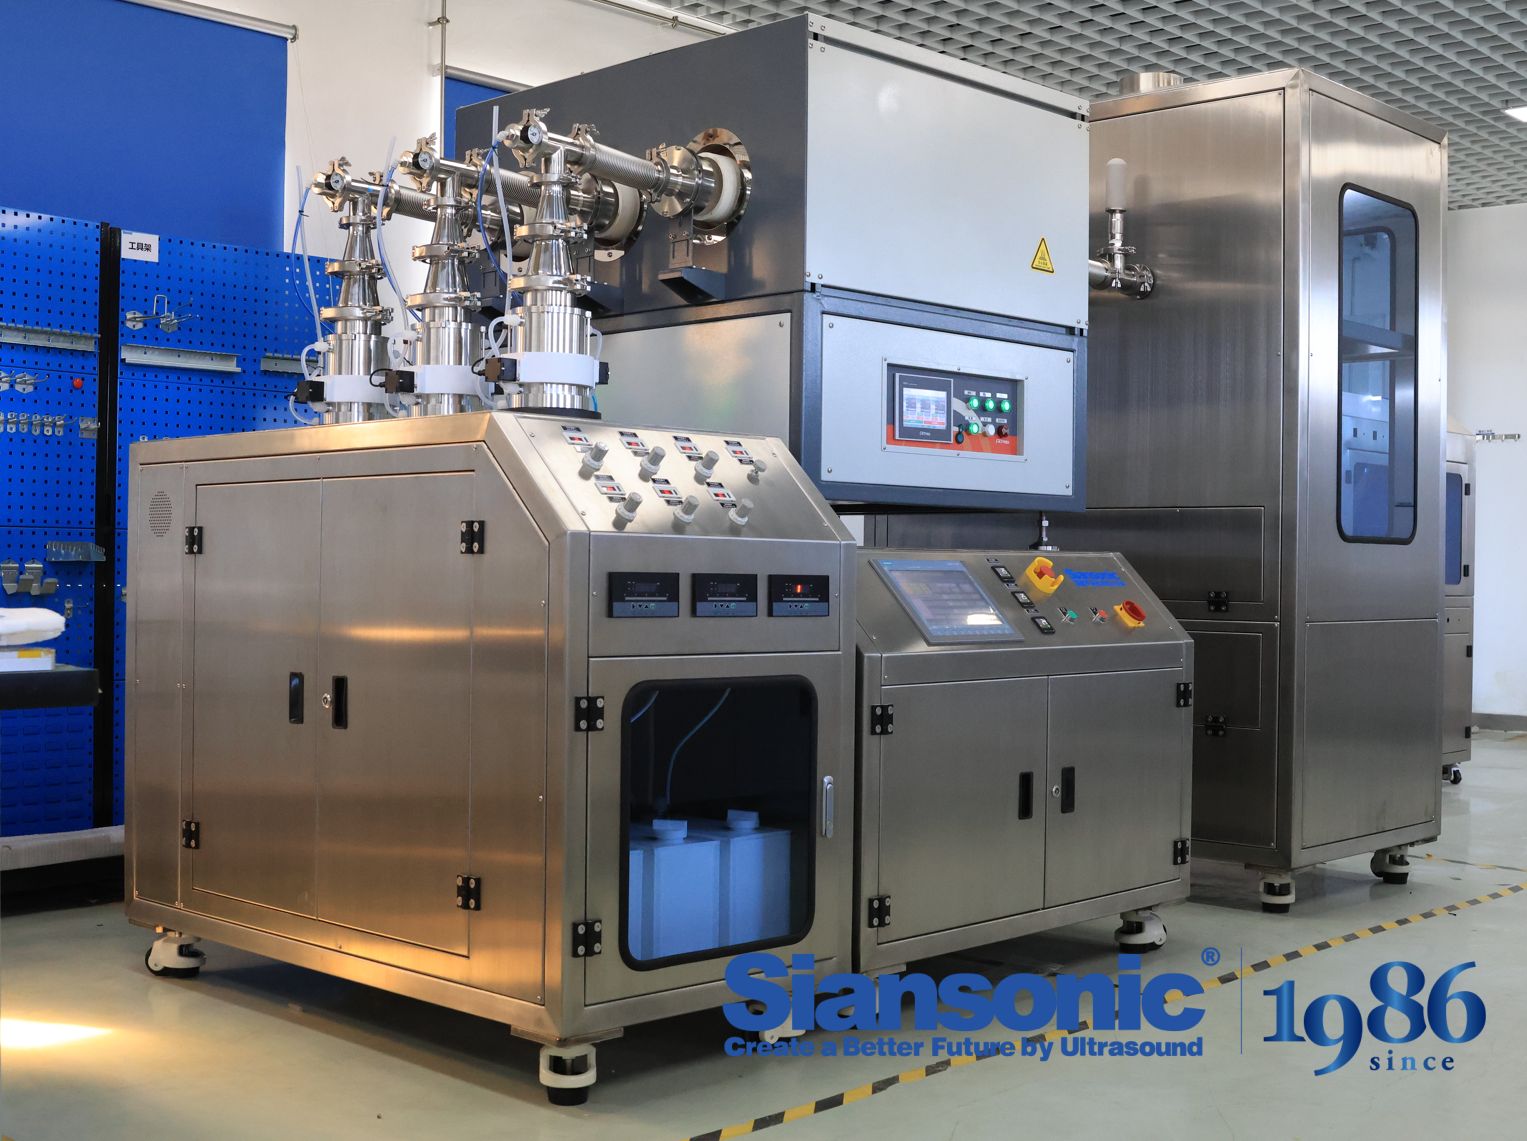
Achieving consistent coating outcomes starts with controlling the variables that most affect atomization and transfer efficiency. Instead of treating pressure and nozzle setup as fixed settings, view them as a dynamic pairing. A slight drop in fluid pressure can alter droplet size and pattern width, while an unchanged air cap may then deliver too much air for the new viscosity. Small, deliberate shifts in one parameter often require a compensating tweak in another, and tracking these adjustments in a simple log reveals patterns that memory alone misses.
Temperature and humidity also play a silent but significant role. Warm solvent evaporates faster, thickening the mixture mid-flight and creating dry spray or orange peel. On humid days, moisture can become trapped under the film, leading to blushing. Rather than chasing the same knob positions every time, observe the fluid's behavior at the gun tip. A two-second test spray on scrap material tells you more about repeatability than any datasheet. Adjust air pressure first, then fine-tune fluid flow, and resist the urge to change both at once.
Finally, document the actual settings that work under specific conditions, not the ideal ones from a manual. Include ambient temperature, batch viscosity, and gun distance. This turns your spray booth into a feedback loop: each adjustment becomes a data point, and repeatable results follow from recognizing patterns rather than repeating numbers blindly. When the next job calls for the same finish, you can dial in a proven starting point and then verify with a quick test panel instead of starting from zero.
Coating Materials That Perform Under Extreme Conditions
Few environments test a coating like the inside of a jet engine, where temperatures swing from subzero at altitude to over 1,000°C within minutes, all while corrosive gases and high-velocity particles hammer the surface. Standard paints or polymer films don’t stand a chance. Instead, engineers turn to ceramic-based thermal barrier coatings, often yttria-stabilized zirconia, applied by plasma spray or electron-beam physical vapor deposition. These layers don’t just resist heat—they actively insulate the underlying alloy, dropping metal temperatures by up to 200°C. That margin means the difference between a turbine blade lasting 10,000 hours or failing catastrophically mid-flight.
But extreme conditions aren’t only about heat. Deep-sea equipment faces 600 bar of pressure, saltwater corrosion, and biofilm buildup, while chemical processing valves endure concentrated acids at boiling points. In these cases, fluoropolymers like PTFE and PFA excel due to their near-universal chemical inertness and low friction, though they can creep under load. For abrasive slurry pipelines, tungsten carbide or chromium carbide hardfacing applied via high-velocity oxygen fuel (HVOF) spraying provides wear resistance that outlasts solid alloy parts by a factor of three to five. The key isn’t finding one miracle material—it’s matching the coating’s failure mode to the specific stress: thermal fatigue, erosion, cavitation, or chemical attack.
Recent advances push the boundaries further. Multi-layer gradient coatings blend ceramic and metal to reduce thermal expansion mismatch and prevent spalling. Self-healing coatings, embedded with microcapsules of polymerizable agents, seal micro-cracks before they propagate. And for space applications, where atomic oxygen erodes most organics and temperature cycles swing 200 degrees in 90 minutes, inorganic silicate binders with ceramic pigments have proven stable for decades on the International Space Station. The common thread is a shift from passive protection to engineered survival—designing the coating not just to sit on a surface, but to adapt, sacrifice, or regenerate under stress that would destroy conventional materials.
Matching System Design to Your Production Scale
A line that produces a few dozen units a week has no business copying the architecture of a plant running three shifts. Small-batch and pilot operations usually get more value from manual workstations, simple roller conveyors, and layouts that can be rearranged in an afternoon. Spending on full automation at this stage often creates a rigid system that fights you during product changes and never earns back its capital.
Once volumes climb into the mid range, the goal shifts to reducing touch time without locking in a single process. Semi-automated cells, standardized mechanical and electrical interfaces, and targeted data collection at known bottleneck points tend to work better than a sprawling control system. Building the line as distinct modules lets you add capacity, swap out a station, or reroute material flow without tearing down everything around it.
High-volume production is where integrated automation, redundancy, and real-time monitoring start to pay for themselves. But even at full scale, the design should protect access for maintenance and rapid changeover. A line that runs at maximum theoretical speed yet takes two shifts to recover from a jam is less productive than a slightly slower system that operators can clear in minutes.
From Lab Prototypes to High-Volume Manufacturing
Scaling a product from a hand-built lab prototype to a line that churns out thousands of units per week is rarely a straight path. The early bench version might rely on 3D-printed brackets, hand-soldered joints, and a microcontroller chosen for convenience rather than cost. Once volume targets enter the conversation, every one of those choices gets revisited. Materials that were fine for five units can become impossible to source at quantity, and assembly steps that took a technician an hour need to be redesigned so a machine or an operator with minimal training can do them in minutes.
The shift usually happens in stages. First comes a manufacturing pilot, where the design is frozen enough to build a few dozen or a few hundred units using the intended production processes. That pilot run surfaces the problems that never show up in the lab: tolerance stack-ups that make housings hard to snap together, test fixtures that can't keep up with the line rate, and suppliers that quote one lead time but deliver in twice that. Each fix feeds back into the design, and the cycle repeats until the yield and takt time look acceptable.
By the time a product reaches true high-volume output, the original prototype often shares little more than its core function with the final version. The goal is no longer just proving the idea works, but proving it can be made consistently, affordably, and quickly enough to meet real demand. That transition demands close cooperation between engineering, sourcing, and operations, and it's where many promising projects either find their footing or quietly stall.
Verifying Film Quality Without Destructive Testing
Assessing film integrity usually means accepting that some samples will be sacrificed, but modern inspection methods allow for thorough quality checks without cutting, stretching, or exposing the material to damaging conditions. Optical profilometry, for instance, maps surface topography at micron-level resolution, catching pinholes, thickness deviations, or coating inconsistencies that would otherwise go unnoticed until failure. Similarly, non-contact ultrasonic testing sends high-frequency waves through the film and reads the echoes to detect internal voids or delamination without leaving a mark on the roll.
What makes these approaches particularly practical is their ability to run inline during production rather than offline on a lab bench. A film line equipped with machine vision cameras and laser micrometers can continuously monitor width, edge quality, and haze in real time, flagging anomalies the moment they appear. This shifts quality control from reactive sampling to proactive process feedback, reducing waste while giving converters confidence that every meter leaving the facility meets the same tight specification as the tested samples.
The real advantage, though, lies in the data trail. Non-destructive tests generate dense, repeatable measurements that can be stored and compared across batches, revealing drift in raw materials or extruder conditions long before defects become visible. When a downstream customer asks for verification, the manufacturer can pull up thickness maps, barrier property readings, or optical clarity scores for the exact roll in question—no need to unspool it, cut a coupon, and hope that tiny piece represents the whole shipment.
FAQ
It relies on high-frequency vibrations to turn the precursor liquid into a fine mist, producing more uniform droplet sizes and better film consistency than pressure-driven nozzles.
Photovoltaics, fuel cells, gas sensors, and medical device manufacturing commonly use these coatings where controlled thickness and surface quality are critical.
Closed-loop control of liquid flow, nozzle travel speed, and substrate temperature is combined with real-time monitoring of droplet size and deposition rate to keep thickness consistent.
Yes, the atomized droplets reach the heated surface gently and the low thermal mass per droplet allows coating without subjecting the whole part to prolonged high heat.
Aqueous solutions, solvent-based formulations, and even nanoparticle suspensions can be processed as long as they can be atomized at the system's operating frequency without nozzle clogging.
Inconsistent films create weak spots in electronic and optical devices. Precise atomization and programmable nozzle paths reduce edge effects, pinholes, and thickness variation.
Routine cleaning of the nozzle tip, checking ultrasonic transducer connections, and scheduled replacement of liquid feed lines help avoid drift and unexpected downtime.
Manufacturers usually offer modular setups ranging from single-nozzle lab units to multi-nozzle inline systems with automated substrate handling, so users can scale without redeveloping the coating process.
Conclusion
Achieving consistent thin-film coatings at scale depends on more than just choosing the right chemistry. The ultrasonic nozzle itself becomes the primary control point for droplet size distribution and impact energy, which directly shapes film uniformity. By modulating frequency, flow rate, and carrier gas, operators can tune deposition to match substrate topography and minimize overspray. A well-designed system also lets you adjust these parameters quickly and store them as repeatable recipes, so the same coating result can be reproduced across shifts or between machines. This repeatability is particularly valuable when working with materials that must survive thermal cycling, corrosive environments, or abrasive wear. Manufacturers who specialize in ultrasonic spray pyrolysis understand that the coating's performance is inseparable from how the aerosol is generated and delivered.
Scaling from benchtop experiments to full production introduces a different set of constraints. Laboratory prototypes often tolerate manual adjustments and short runs, but high-volume manufacturing demands closed-loop control, uniform exhaust, and reliable substrate handling. A capable manufacturer matches the system footprint, conveyor speed, and nozzle array to the required throughput without sacrificing edge uniformity or film thickness tolerance. Equally important is quality verification. Non-destructive methods such as spectral reflectance, ellipsometry, or automated visual inspection can flag coating defects early, preventing scrap and reducing the need for destructive cross-sectioning. By integrating these measurement tools into the line, engineers gain confidence that every part leaving the spray zone meets the same electrical, optical, or protective specifications. This combination of precise aerosol generation, scalable hardware design, and inline metrology is what separates a true precision coating partner from a generic spray equipment supplier.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/